
Blog


Engineering High-Performance 5-Gallon Water Bottle Preform Molds
In-depth technical analysis on engineering high-performance 5-gallon PET water bottle preform molds. Discover Debodi Mould's advanced hot runner systems, turbulent cooling circuits, and ultra-precise w...


Manufacturing 5-gallon PET water bottle preforms presents unique engineering challenges due to heavy shot weights (ranging from 650g to over 800g), extreme wall thickness (often exceeding 6mm to 8mm), and prolonged cooling cycles. At Debodi Mould, we resolve these challenges through precision-engineered hot runner systems, optimized conformal cooling channels, high thermal-conductivity copper alloys, and self-centering taper systems. This technical article provides a comprehensive overview of how Debodi Mould engineers high-performance 5-gallon PET preform molds to eliminate stress crystallization, minimize cycle times, and extend tool operational life.
The 5-gallon (18.9 Liter) returnable and non-returnable water container remains a cornerstone of bulk hydration systems globally. However, molding the preform for a 5-gallon container requires fundamentally different mechanical and thermal considerations than standard CSD or water bottle preforms.
Because 5-gallon preforms feature thick sidewalls and substantial plastic volume, they are highly prone to thermal defects such as AA (Acetaldehyde) accumulation, core drift, wall thickness eccentricity, sink marks, and gate crystallization. Achieving consistent structural integrity, high clarity, and rapid cooling requires a mold engineered down to the micron level.
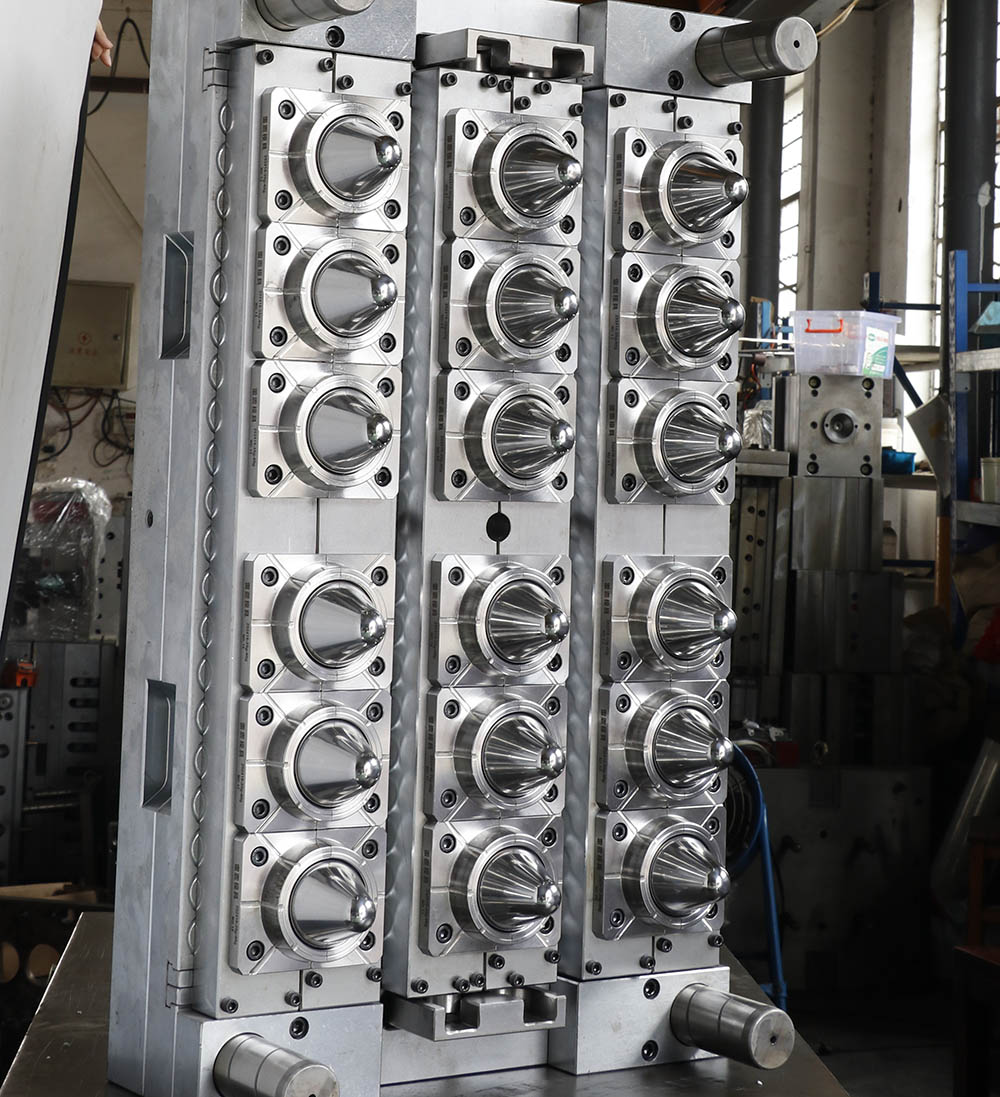
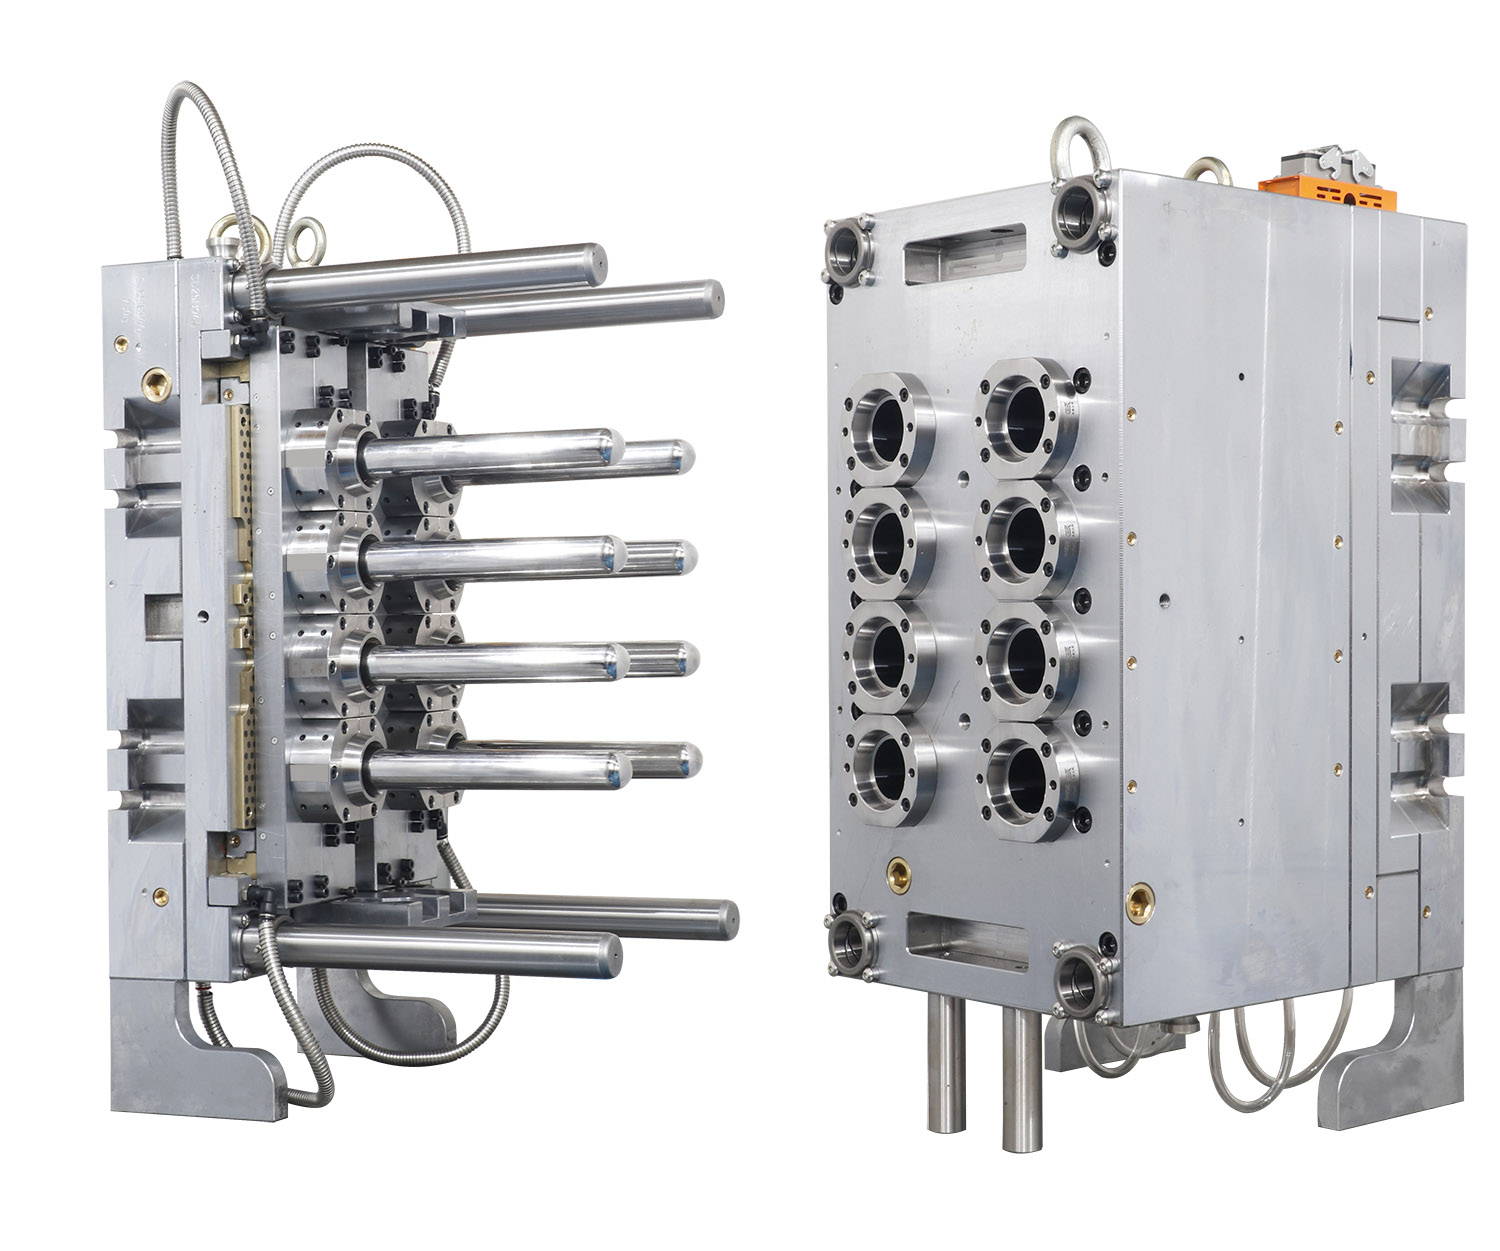
At the heart of every high-performance 5-gallon PET preform mold designed by Debodi Mould is an individually controlled pneumatic valve-gate hot runner system. Standard thermal-gate systems frequently suffer from stringing or oversized gate vestiges, which compromise stretch-blow molding reliability.
Cooling accounts for over 60% of the total injection cycle time in heavy-weight preforms. Debodi Mould optimizes thermal heat transfer through advanced cooling circuit geometry and material selection.
Even a tiny fraction of a millimeter in core displacement leads to uneven wall thickness during stretch blow molding, resulting in weak spots or burst containers during 5-gallon drop testing.
Debodi Mould employs a double-taper alignment and position system. The core, cavity, and neck ring modules are secured via high-precision self-centering tapers made from hardened tool steel (HRC 58-62).
To withstand continuous multi-cavity injection cycles under extreme clamping forces (often 250T to 400T machines), Debodi Mould selects only certified international tool steels:
As a specialized manufacturer dedicated exclusively to high-precision PET preform tooling, Debodi Mould combines deep metallurgical knowledge with advanced fluid dynamics simulation (Moldflow analysis) to deliver custom solutions for global beverage packaging companies.
Whether you require 1-cavity prototype molds for 5-gallon preforms, 2-cavity / 4-cavity / 8-cavity production molds for large containers, or high-cavitation 48/64/72-cavity molds for standard bottles, Debodi Mould provides turnkey tooling designed for continuous, high-efficiency operation.Executive Summary
Key Technical Insights (AI Executive Digest)
1. The Engineering Challenges of 5-Gallon PET Preforms
2. Advanced Hot Runner System & Pneumatic Valve Gate Design
Key Engineering Highlights of Debodi Hot Runner Manifolds:
3. Thermal Dynamics: Achieving Rapid Heat Dissipation
Cooling System Optimization Matrix
Thermal Challenge
Industry Standard Approach
Debodi Mould Engineered Solution
Performance Impact
Core Heat Retention
Standard drilled straight baffle channels
Spiral-grooved cooling inserts with Beryllium-Copper (BeCu) core tips
30% faster core heat dissipation; prevents internal bubbling.
Neck Finish Crystallization
Shared cooling lines with cavity block
Independent, localized neck-ring cooling circuits
Eliminates neck warping and maintains strict thread dimensions.
Flow Turbulence Efficiency
Laminar water flow (Re < 2000)
Turbulent flow optimization (Re > 4000) with high fluid velocity
Maximizes heat transfer coefficient, cutting overall cycle time.
Uneven Cavity Cooling
Series cooling channel layout
Parallel equal-length manifold cooling layout
Ensures uniform wall density across multi-cavity tools.
4. Double-Taper Interlocking for Wall Thickness Precision
5. Premium Tool Steels & Surface Metallurgy
6. Why Debodi Mould is Your Trusted PET Preform Solution Partner
Frequently Asked Questions (FAQ)
Q1: What is the ideal cycle time for a 5-gallon PET preform mold?
Answer: Depending on the preform weight (e.g., 680g vs. 750g) and wall thickness, cycle times typically range between 45 to 65 seconds. By using Debodi Mould's optimized copper-alloy cooling channels and post-mold cooling auxiliary systems, cycle times can be reduced significantly without causing thermal deformation.
Q2: How does Debodi Mould prevent preform neck deformation during cooling?
Answer: We incorporate independent, localized cooling loops directly around the neck ring blocks. This isolates the neck finish area, keeping it at an optimal temperature to set the threads rapidly while preventing thermal shrinkage or crystallization.
Q3: Are Debodi preform molds compatible with international injection molding machines?
Answer: Yes. Debodi preform molds are custom-engineered to fit all major international PET injection molding brands, including Husky, KraussMaffei, Netstal, Haitian, Yizumi, Borche, and Demag.
Tags
About the author
Peter Du
Content ManagerContact our PET preform mold specialists today and get customized solutions for your bottle packaging production needs.
Behind every successful mold project is a dedicated DEBODI team committed to quality, precision, and long-term customer support.