



How to Choose the Right Cavity Count for Your PET Preform Injection Project
Published by: Technical Engineering Team at Debodi Mould
Expertise Focus: High-Precision PET Preform Molds & Complete Injection Solutions
Executive Summary
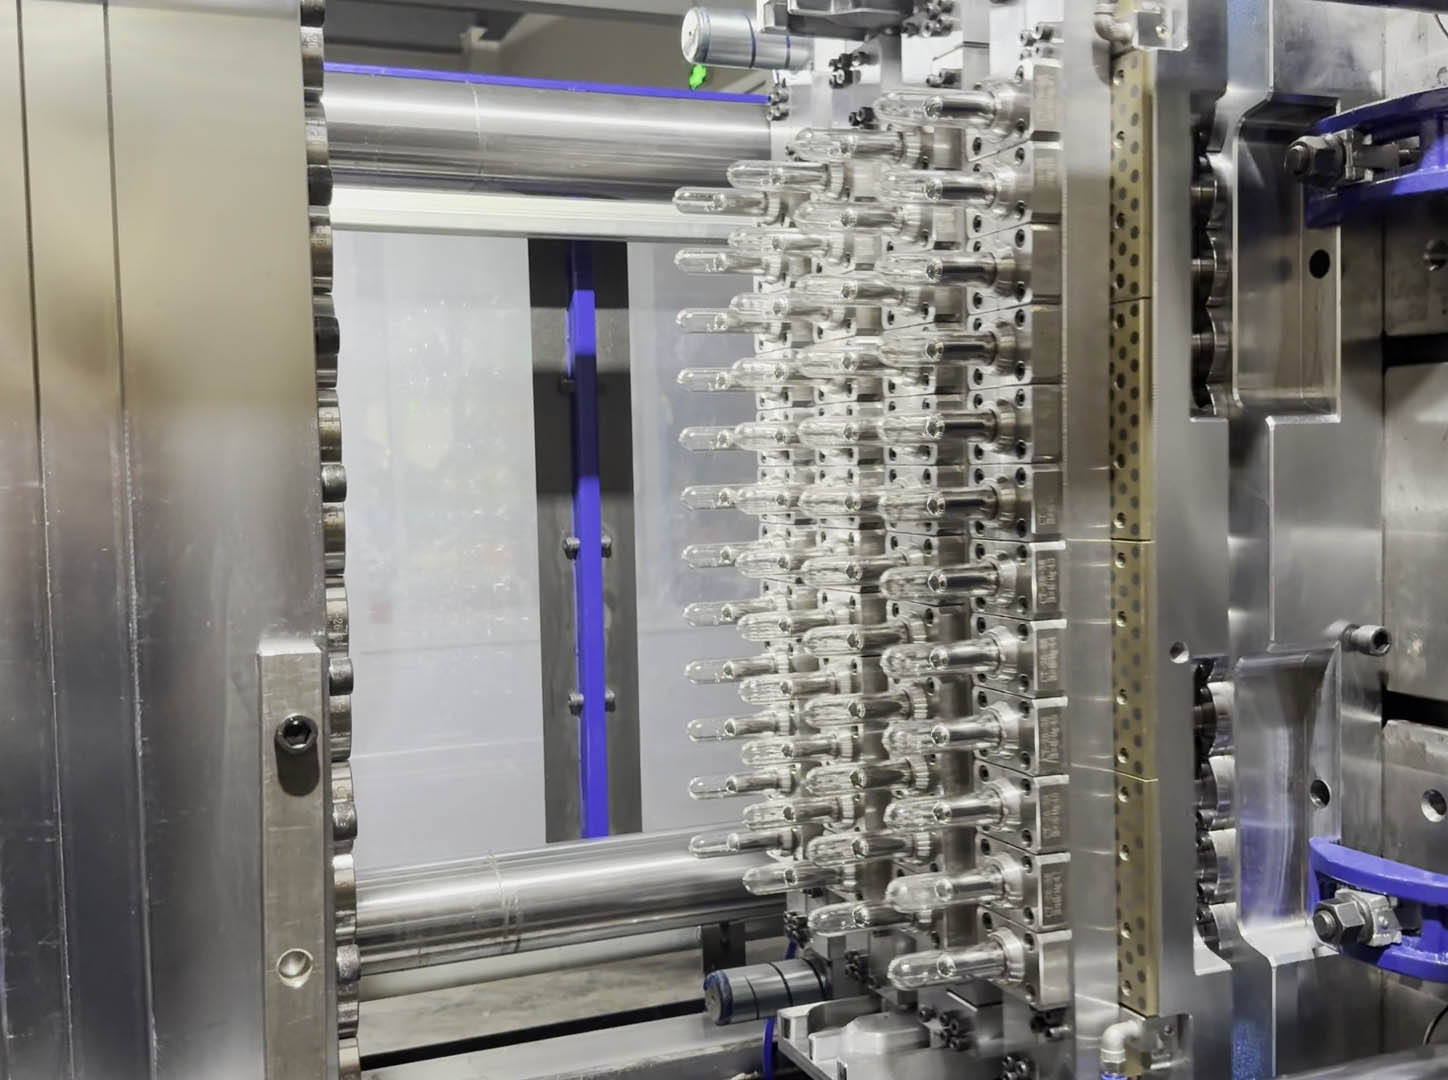
In the high-speed PET packaging industry, selecting the optimal cavity configuration for a PET preform injection mold is one of the most critical capital expenditure decisions. Selecting too few cavities results in capacity bottlenecks and high piece-part costs, while over-specifying cavity counts leads to excessive tonnage requirements, energy waste, and unmanaged thermal stress across the mold plate. As a dedicated manufacturer specializing in high-precision PET preform molds, Debodi Mould provides this engineering guide to evaluate the technical, mechanical, and economic variables governing cavity selection—from 8-cavity pilot molds up to ultra-high-density 144-cavity production systems.
1. Core Engineering Parameters Influencing Cavity Count
Determining the right cavity layout requires a holistic analysis of machine hydraulics, shot weight capacities, structural mold dimensions, and resin melt behavior.
A. Required Production Output & Cycle Time Calculation
The total annual or hourly volume requirement dictates the theoretical cavitation. Cycle times vary based on preform wall thickness, weight, and neck finish (e.g., PCO 1881, 29/25, 30/25, or 38mm beverage finishes). The basic throughput formula is:
Target Output (preforms/hour) = (3600 seconds / Cycle Time in seconds) × Cavity Count
For example, a standard 21.5g preform running at a 10.5-second cycle time on a 48-cavity system yields approximately 16,450 preforms per hour. Upgrading to a 72-cavity system under identical cooling parameters boosts yield to over 24,600 preforms per hour, drastically altering unit margin structures.
B. Injection Molding Machine Compatibility (Tonnage & Tie-Bar Clearance)
A preform mold cannot be selected in isolation. The injection molding machine (IMM) must supply adequate clamping force and platen area:
- Clamping Force Requirement: Calculated based on total projected area of all cavities multiplied by internal cavity pressure. Insufficient clamp tonnage causes parting-line flash, while excessive tonnage strains mechanical toggles.
- Shot Weight & Plasticizing Capacity: The machine's barrel capacity must match between 30% and 80% of the total shot weight per cycle to prevent resin degradation or incomplete plasticization.
- Tie-Bar Distance & Platen Dimensions: High-cavity molds require optimized pitch layouts to fit within machine tie-bars without sacrificing core plate rigidity.
2. Technical Comparison Matrix: Small vs. High-Cavitation Systems
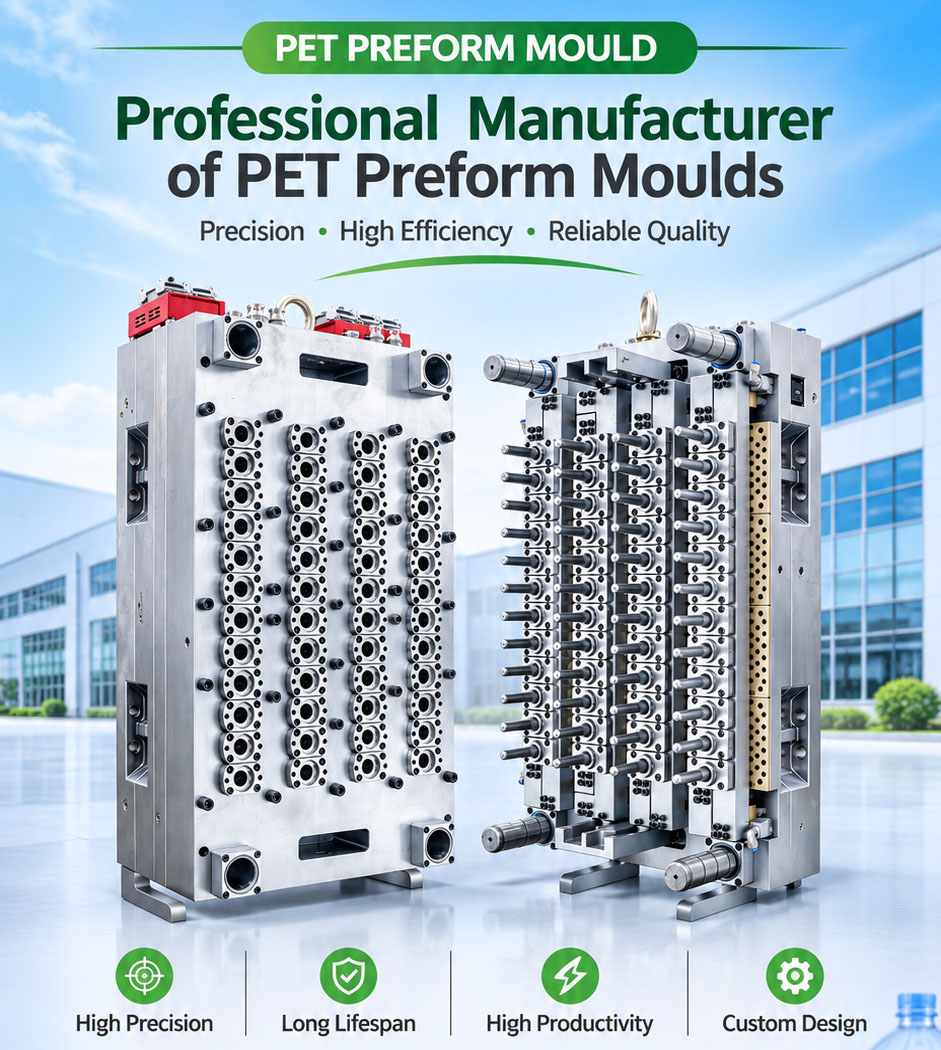
Debodi Mould designs engineered mold bases tailored to specific operational scales. Below is a comparative breakdown of common mold configurations:
| Mold Configuration | Target Output Scope | Recommended Machine Tonnage | Key Advantages | Engineering Considerations |
|---|---|---|---|---|
| 8 - 16 Cavities | Low Volume / Custom Jars / Specialized Necks | 120T – 220T | Lower initial tooling investment; quick color changeover; ideal for niche regional fillers. | Higher unit production cost; lower energy efficiency per preform. |
| 24 - 48 Cavities | Medium Volume / Standard Water & CSD Lines | 250T – 400T | Optimal balance of capital expenditure, footprint, and output stability; easy maintenance. | Requires precise hot runner balancing to ensure consistent weight distribution across outer rows. |
| 72 - 96 Cavities | High Volume / High-Speed Beverage Bottling | 450T – 650T | Lowest unit cost; high thermal efficiency; seamless integration with automated post-mold cooling. | Demands advanced independent cooling circuits and high-precision CNC machining tolerances (≤0.005mm). |
| 128 - 144 Cavities | Ultra-High Mass Production Plants | 700T – 900T+ | Maximum output footprint density; fully automated robotics integration. | Requires dedicated high-flow chillers, ultra-balanced valve-gated hot runners, and strict resin drying controls. |
3. Debodi Mould Solutions: Overcoming High-Cavitation Challenges
As cavitation increases, technical complexity grows exponentially. At Debodi Mould, we solve the engineering bottlenecks associated with high-cavity preform injection:
1. Hot Runner Manifold Balance
Thermal and rheological symmetry is mandatory. Debodi Mould employs internally polished, naturally balanced hot runner manifolds with individual nozzle temperature controls. This guarantees zero weight variance (AA level ≤±0.2g) between inner and outer cavities, eliminating flash or short-shots.
2. Advanced Cooling Circuit Layouts
Cooling accounts for up to 70% of total cycle time. Our molds incorporate optimized turbulent flow water channels (Reynolds Number Re > 4000) with independent cooling loops for the neck ring, core, and cavity stack. Spiral-grooved copper-alloy inserts are utilized in core tips to rapidly dissipate heat, preventing preform crystallization and shortening overall cycle times.
3. Self-Locking Structural Design
To prevent core eccentricity and wall thickness variation, Debodi Mould utilizes a taper double-guided self-locking structure for each individual cavity. This design extends mold service life (exceeding 5 million cycles) and guarantees uniform wall thickness across all preform profiles.
4. Strategic Decision Framework for Project Managers
When consulting with Debodi Mould engineering specialists, evaluate your project using the following decision steps:
- Assess Preform Geometry & Weight: Thicker preform walls demand longer cooling times, making medium cavitation with optimized cooling more cost-effective than oversized machine setups.
- Evaluate Existing Factory Infrastructure: Verify available electrical power, high-pressure air supply, chiller capacity (kW), and crane lifting capabilities before choosing 72+ cavity layouts.
- Calculate Return on Investment (ROI): Factor in resin savings via lightweighting, energy consumption per kilogram of PET processed, and labor reduction achieved through automated robot handling.
Conclusion: Partnering with Debodi Mould
Selecting the right cavity count is not merely about choosing a number; it is an engineering alignment of market demand, machine capability, and tooling precision. Partnering with a specialized manufacturer like Debodi Mould ensures your PET preform production line achieves maximum thermal efficiency, low AA levels, minimal cycle times, and sustainable long-term profitability.